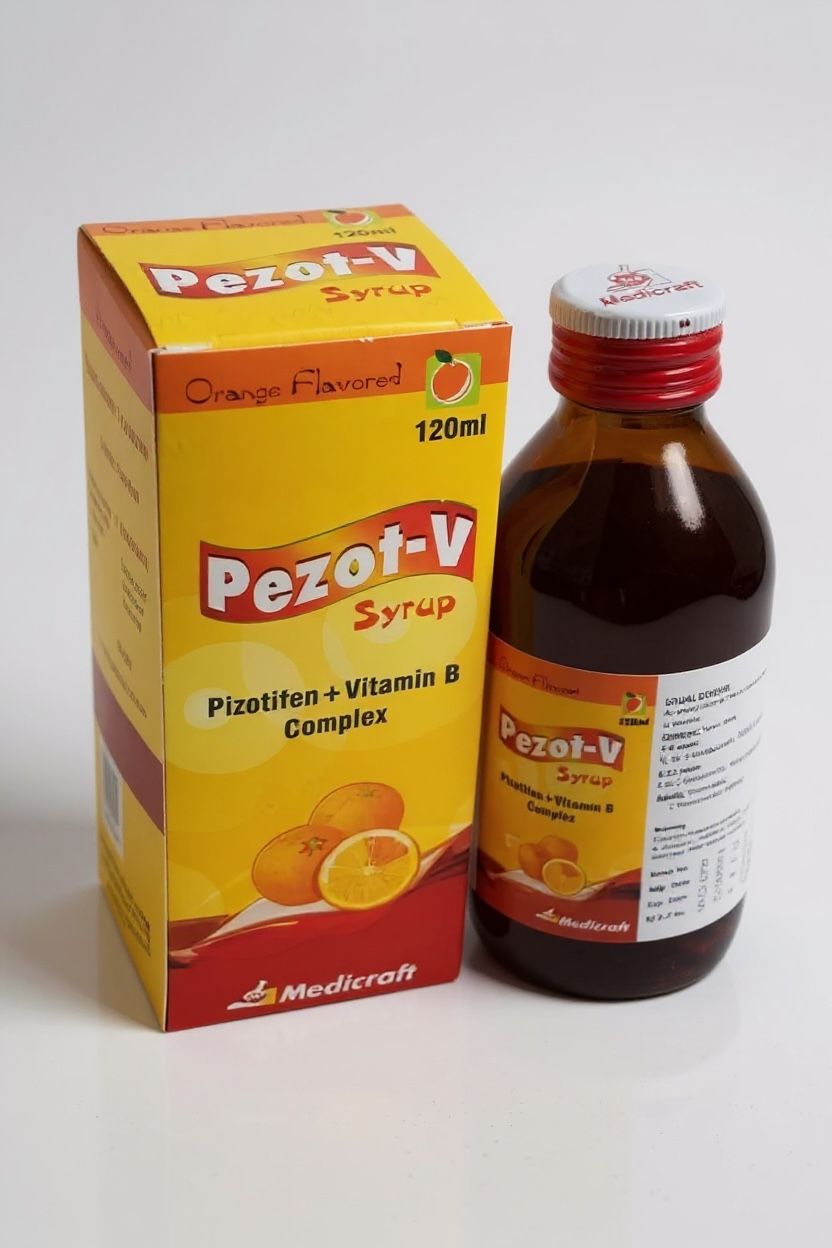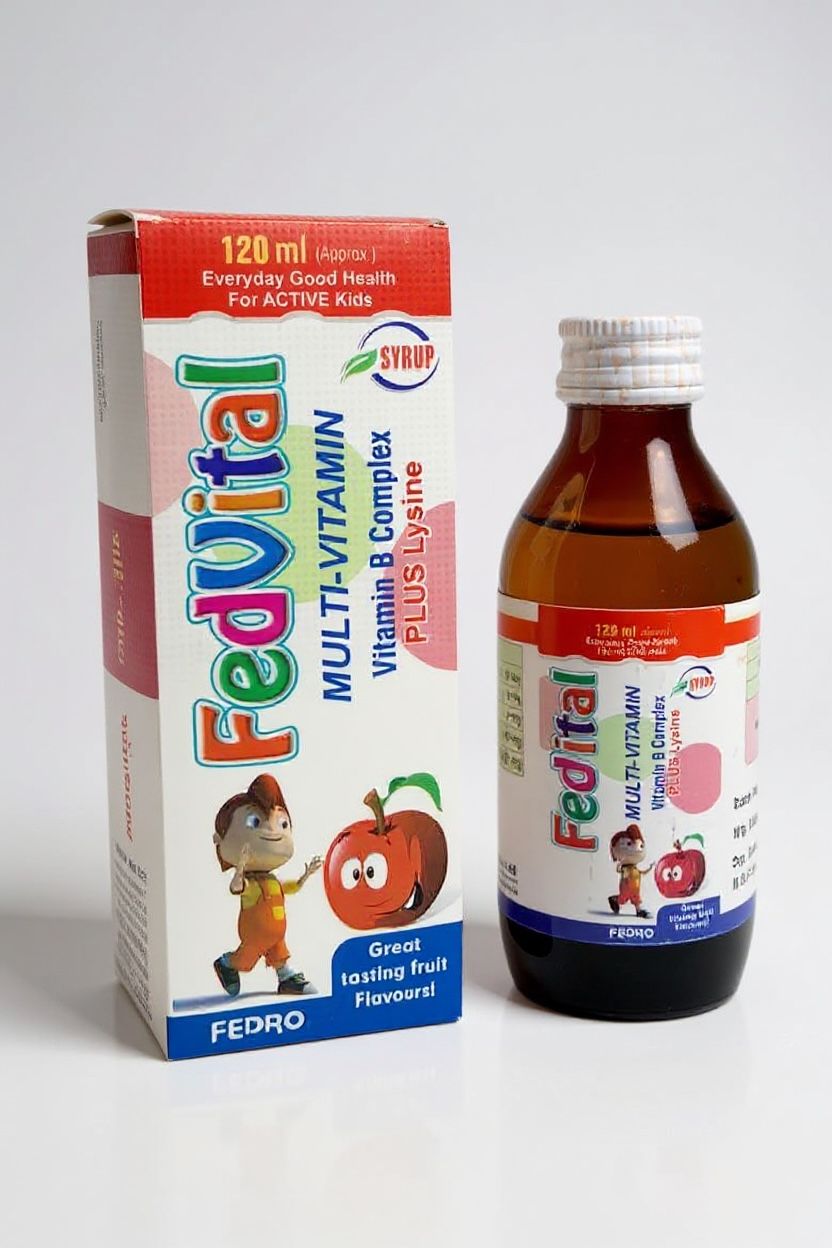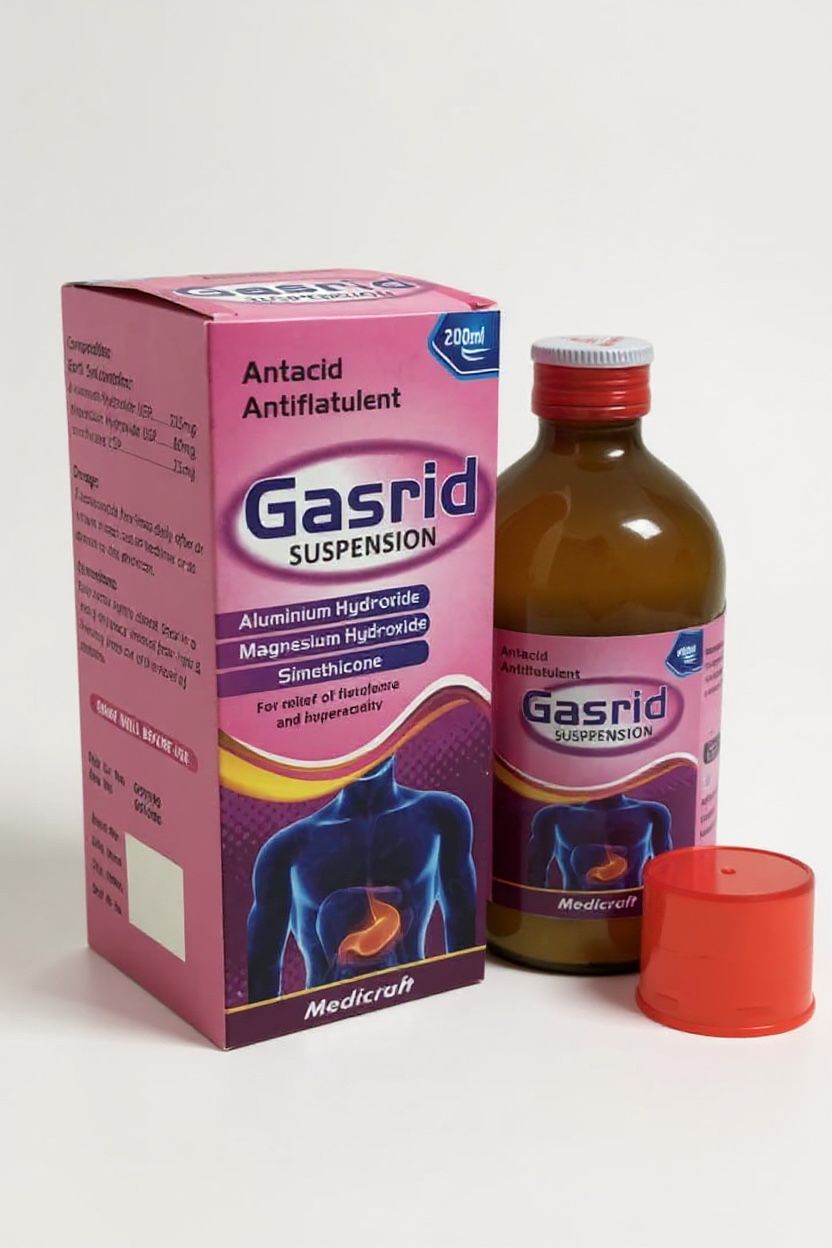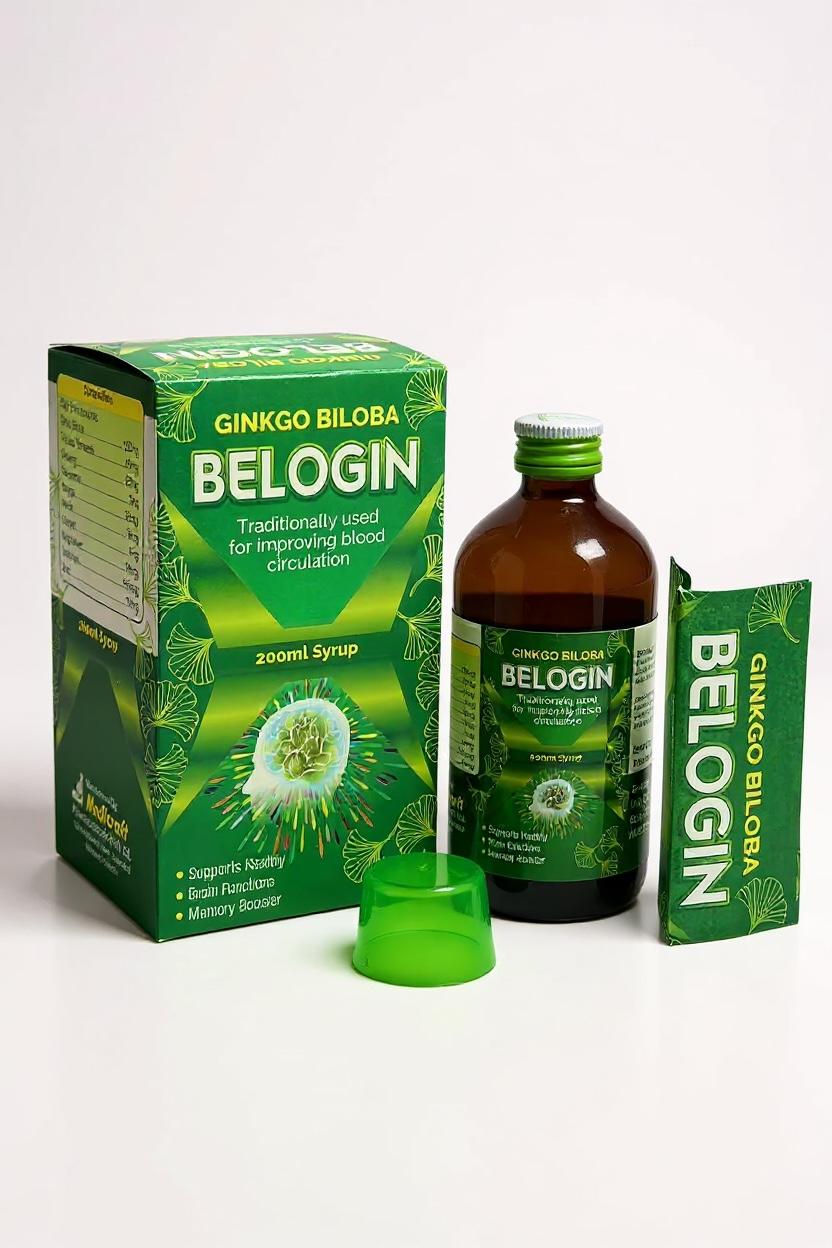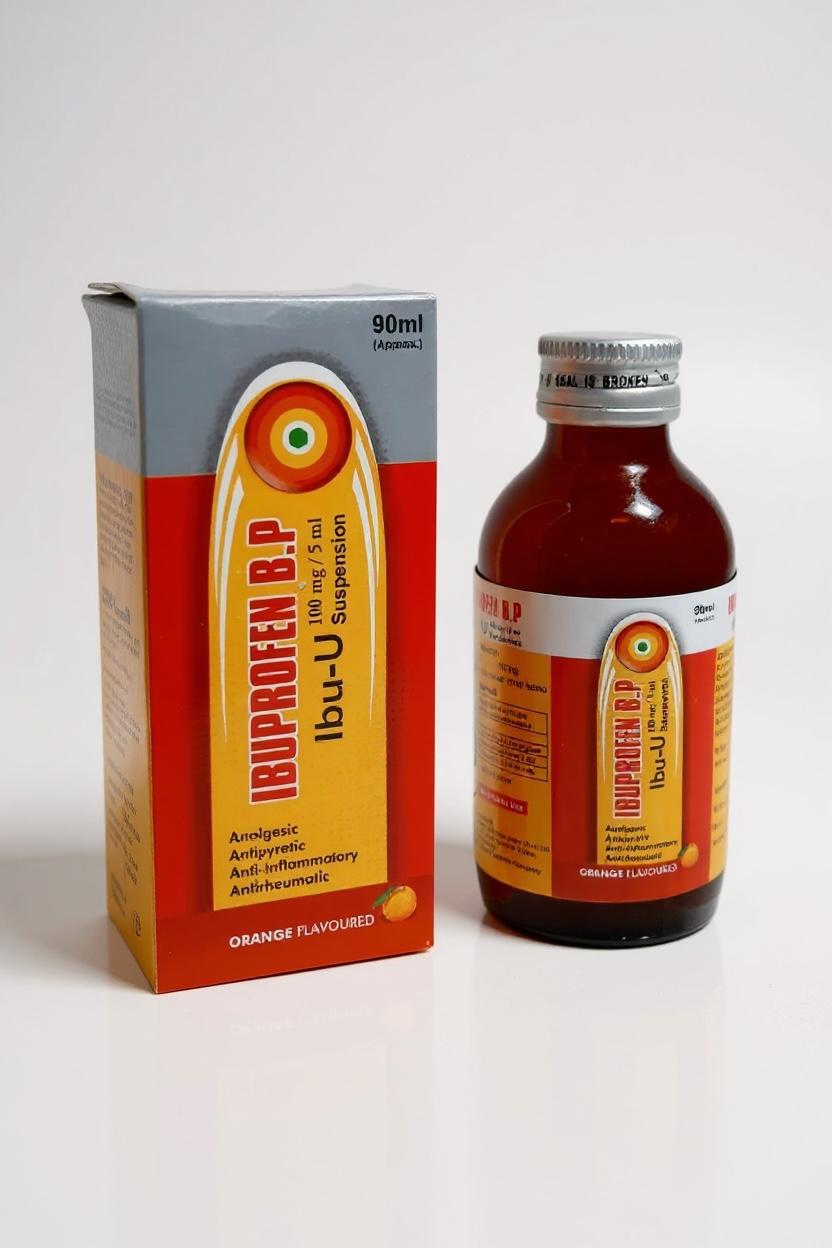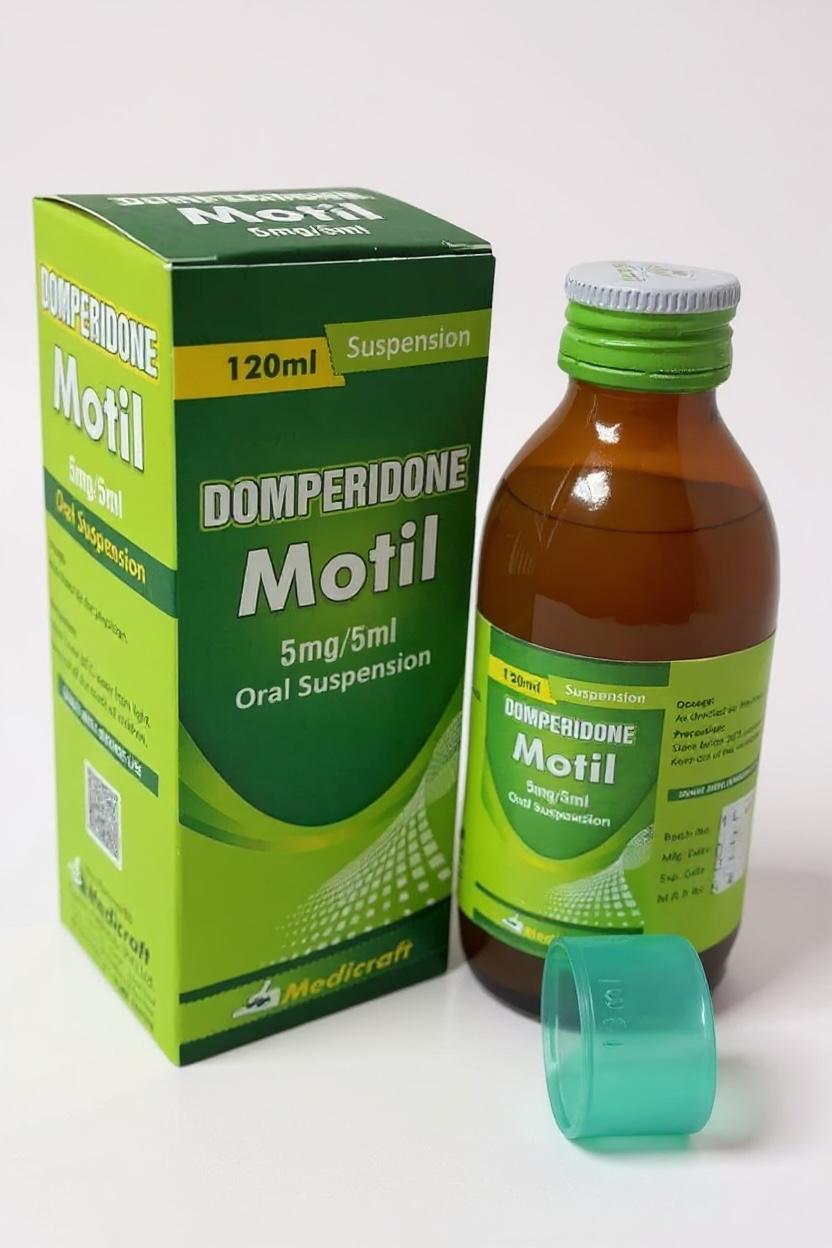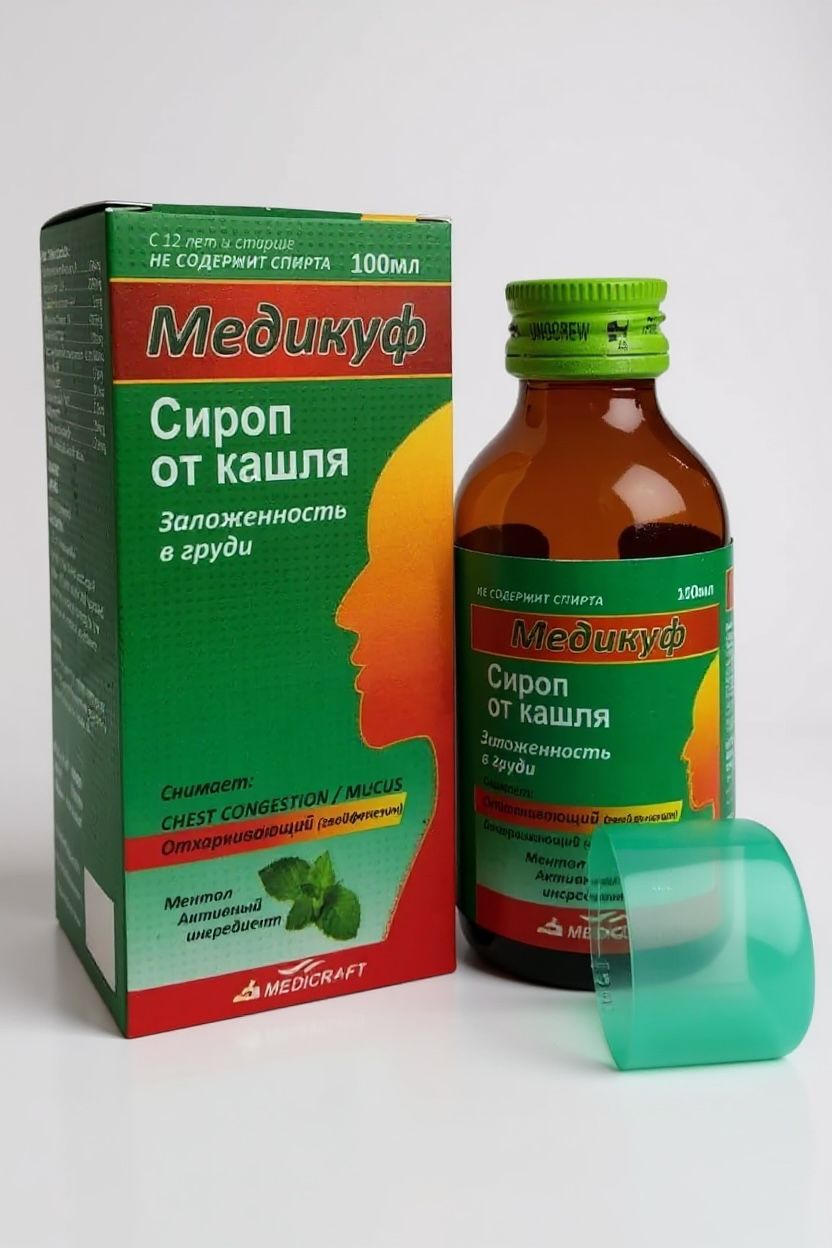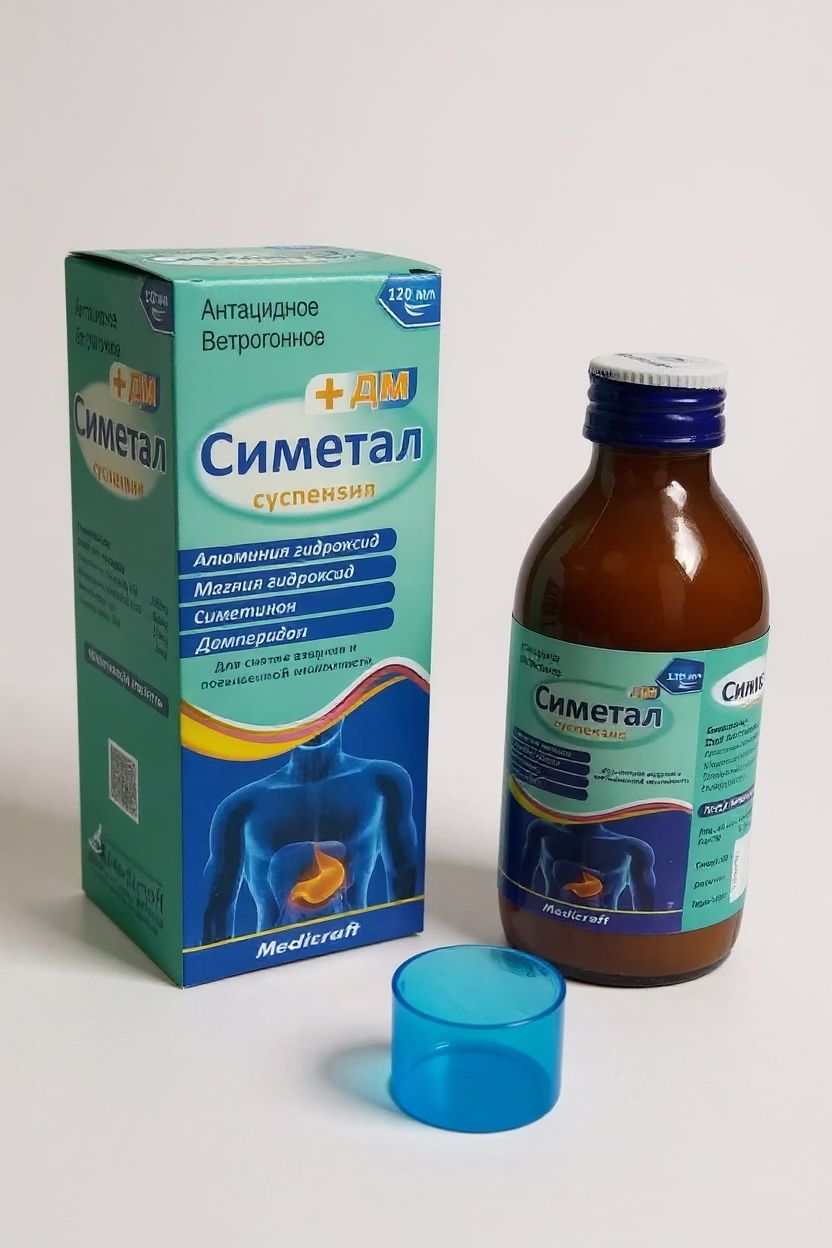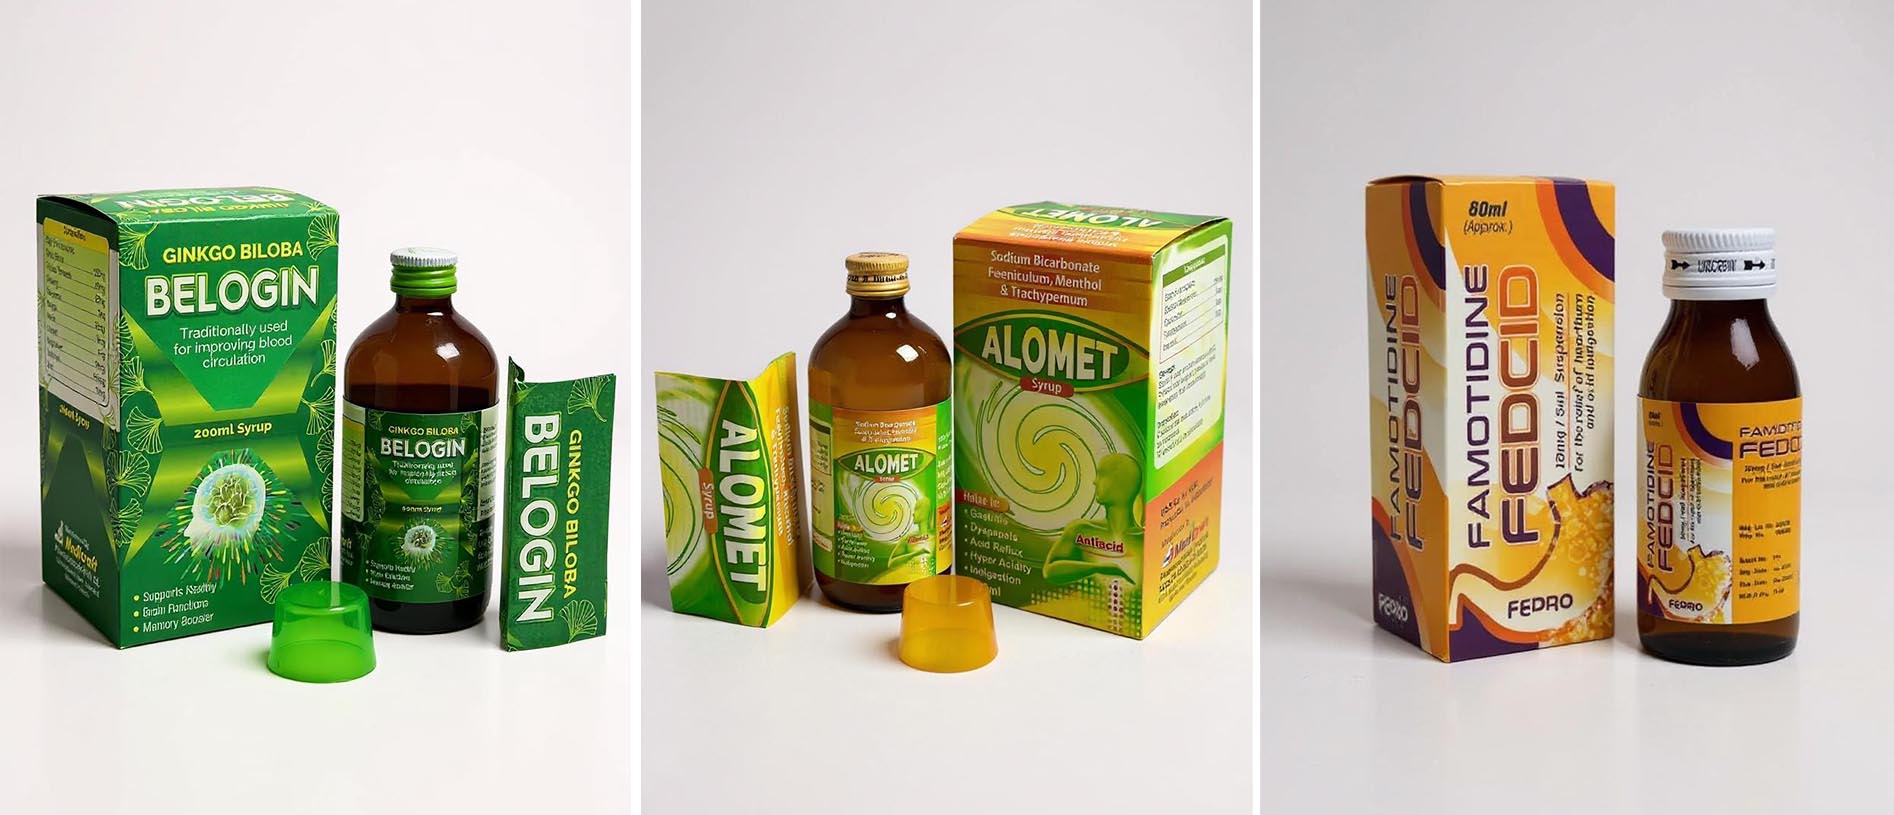
Formulation Excellence and Technology
Every liquid syrup we offer is developed through a multi-step formulation process. The active pharmaceutical ingredients are blended with high-grade excipients, sweeteners, and stabilizers to achieve the perfect balance between efficacy, safety, and taste.
We utilize state-of-the-art mixing and homogenization equipment to offer uniform dispersion of the active ingredients, eliminating sedimentation and dose inconsistency.
Moreover, our R&D partners continuously improve formulations to enhance bioavailability and shelf stability, minimizing degradation over time.
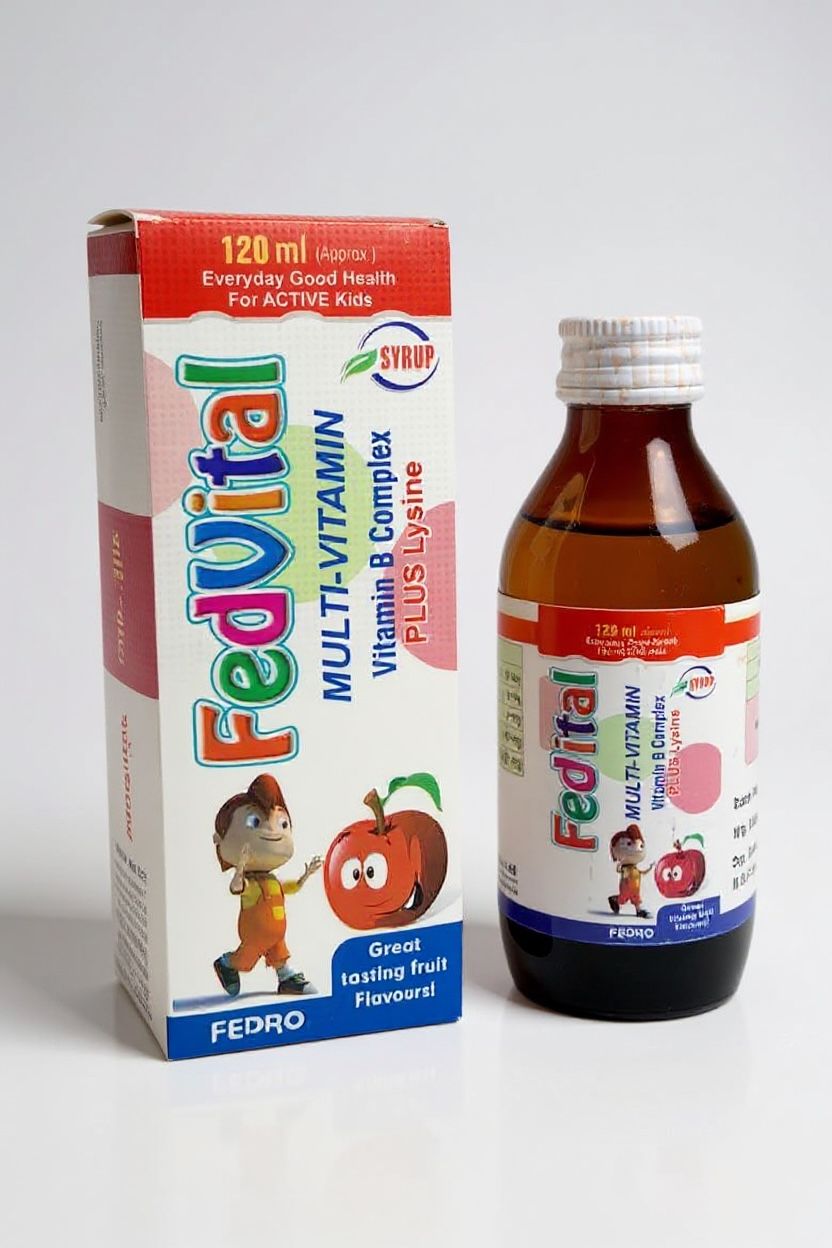
Stringent Quality Assurance
We believe that the foundation of safe pharmaceuticals lies in quality control. Our liquid syrups are produced in WHO-GMP and ISO-certified facilities, offering adherence to international manufacturing standards.
Our testing parameters include:
- Assay and potency tests to confirm accurate API concentrations.
- Microbial limit testing to guarantee sterility.
- Viscosity and pH balance to provide physical stability.
- Accelerated and real-time stability testing for shelf-life validation.
All formulations are lab-tested under varying climatic conditions to confirm their durability and stability, an essential measure for providing reliability across regions with diverse environmental conditions such as Afghanistan, Pakistan, Kyrgyzstan, and Tajikistan.
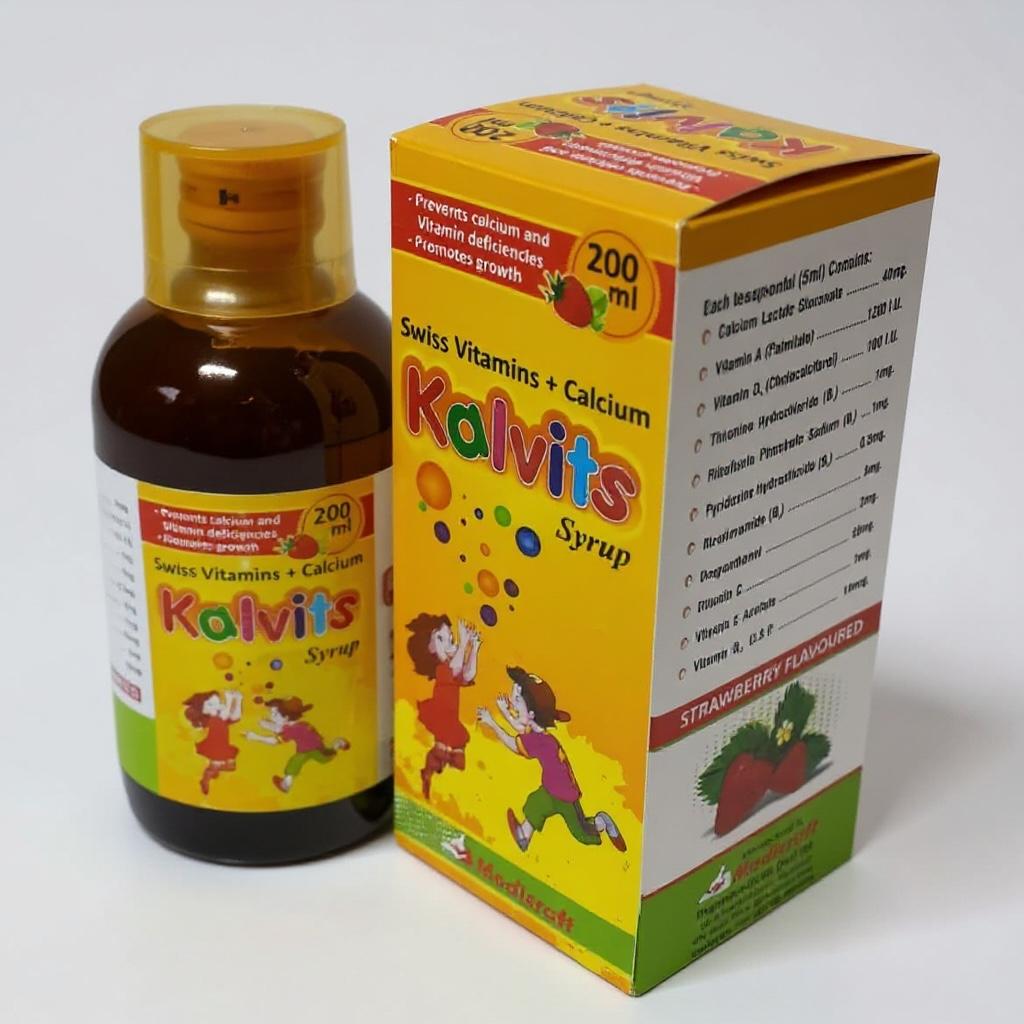
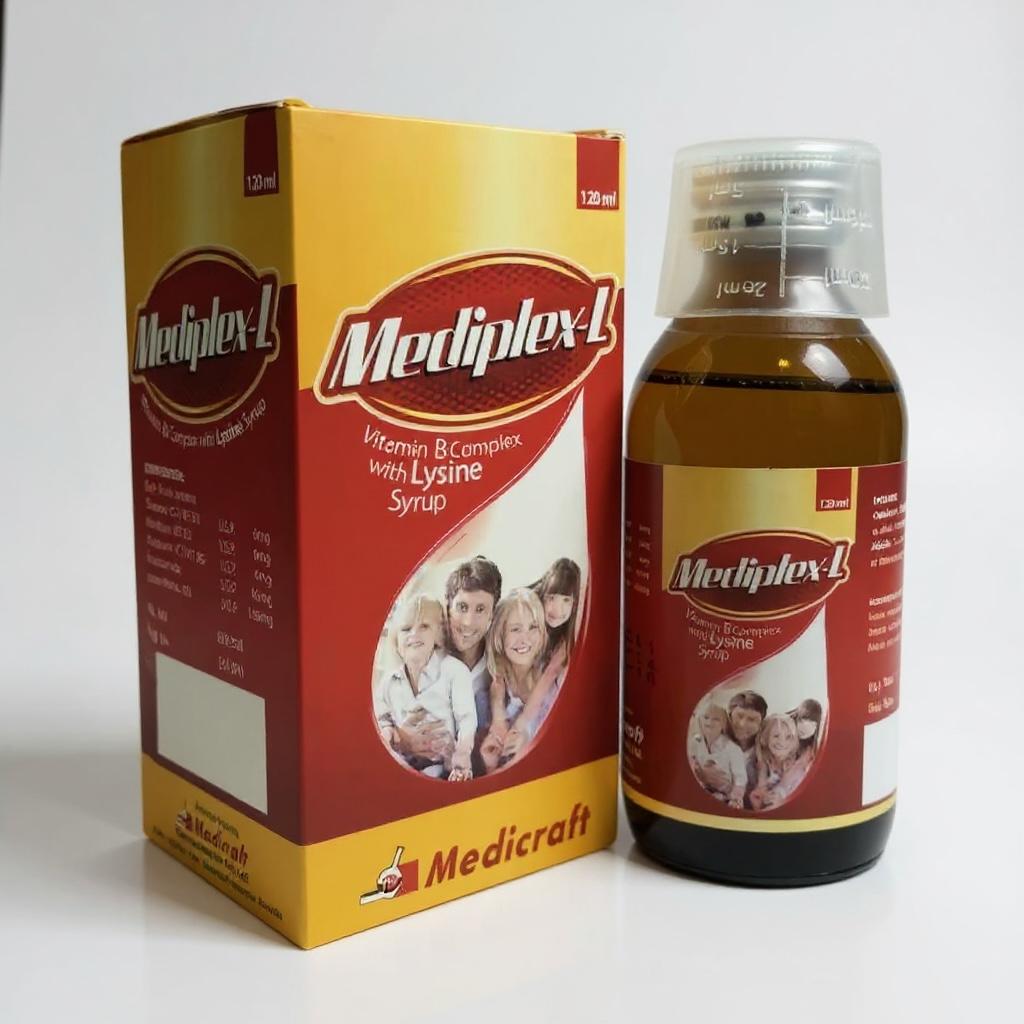
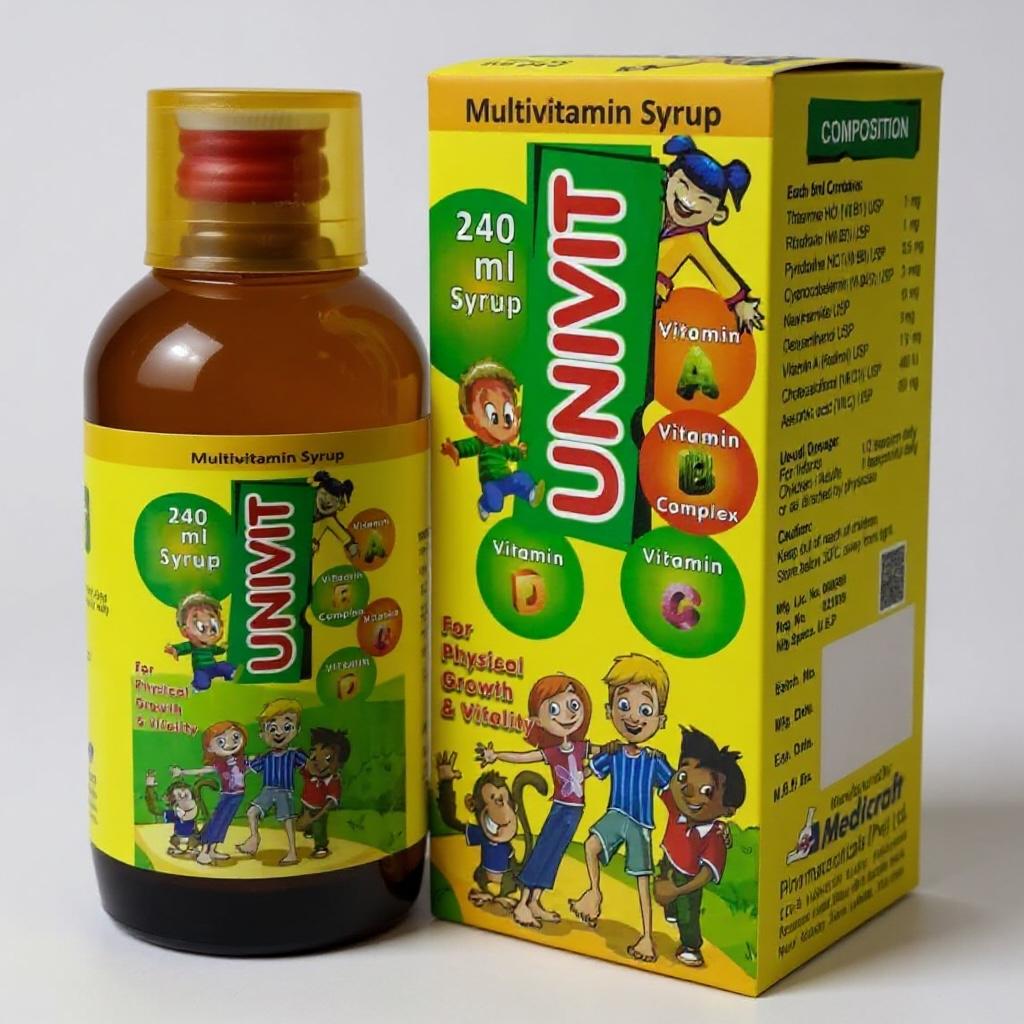
Packaging and Safety Design
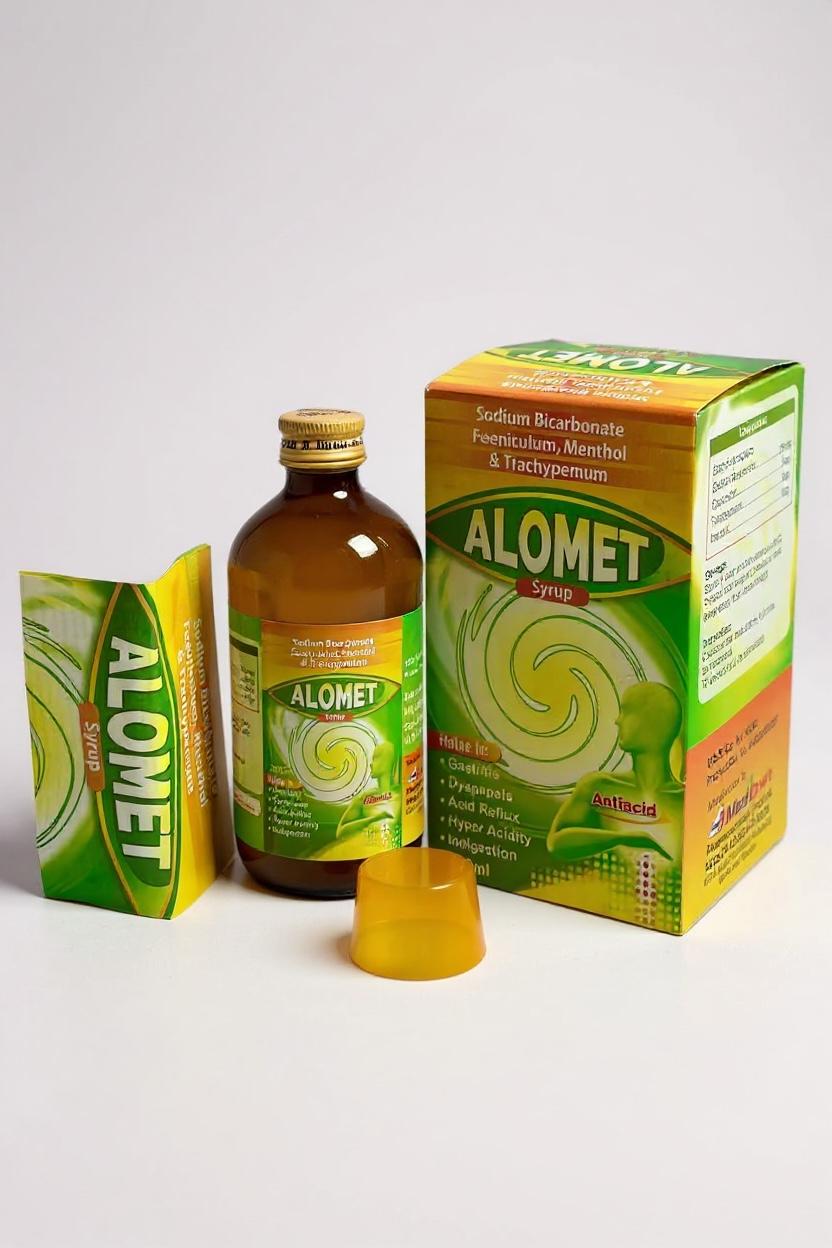
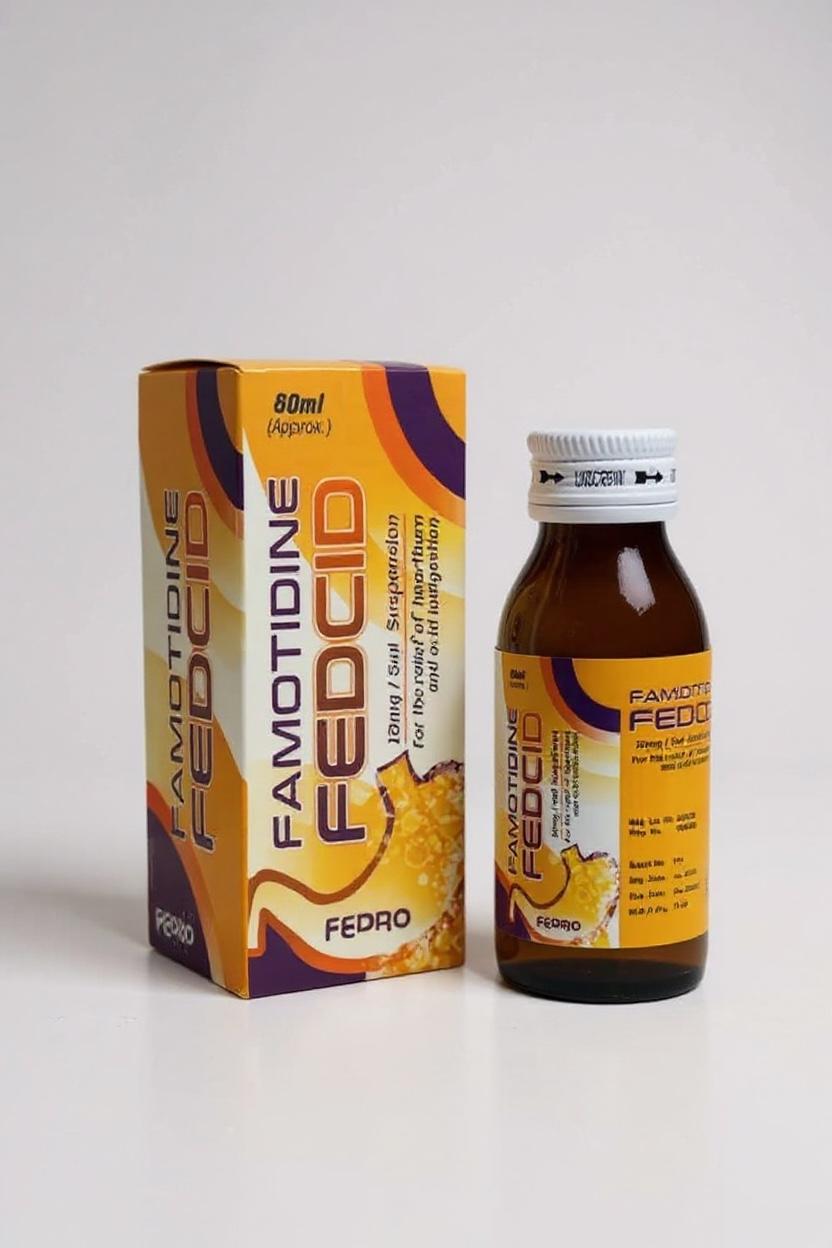
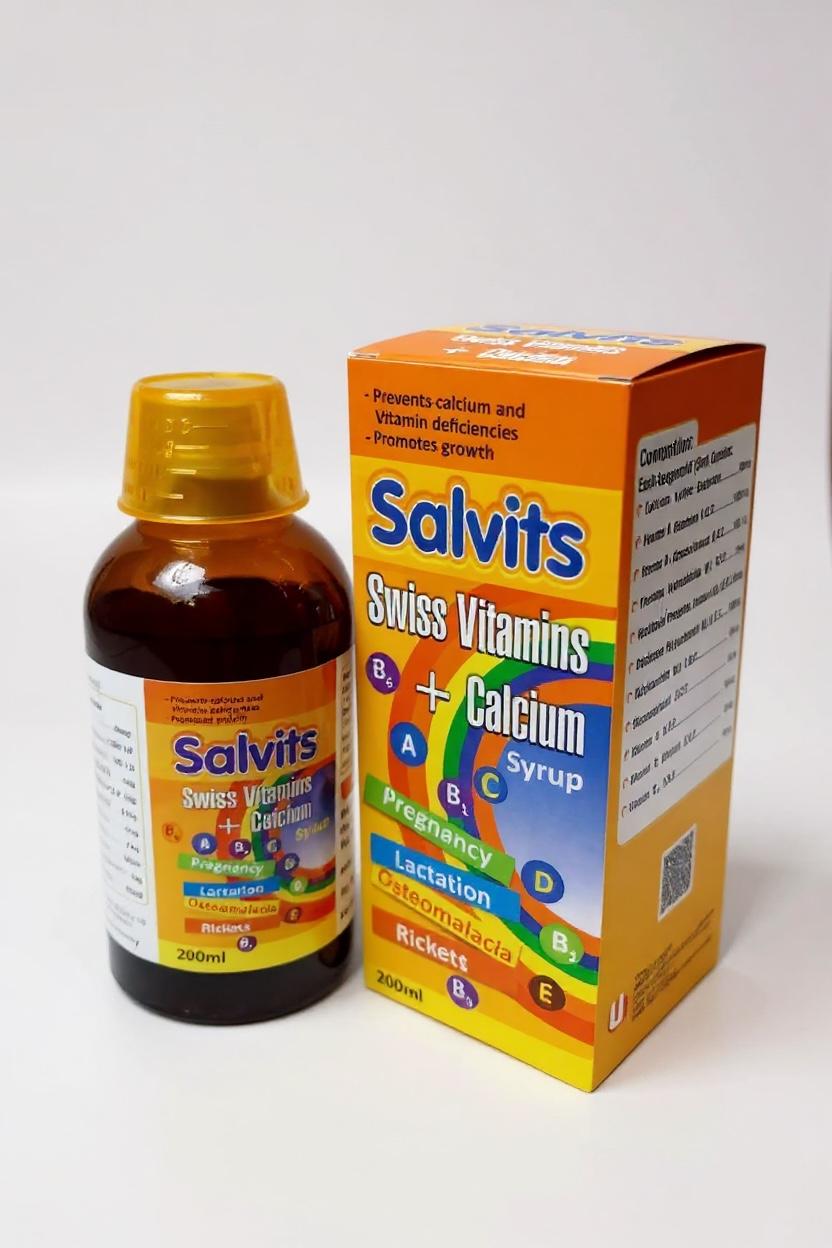
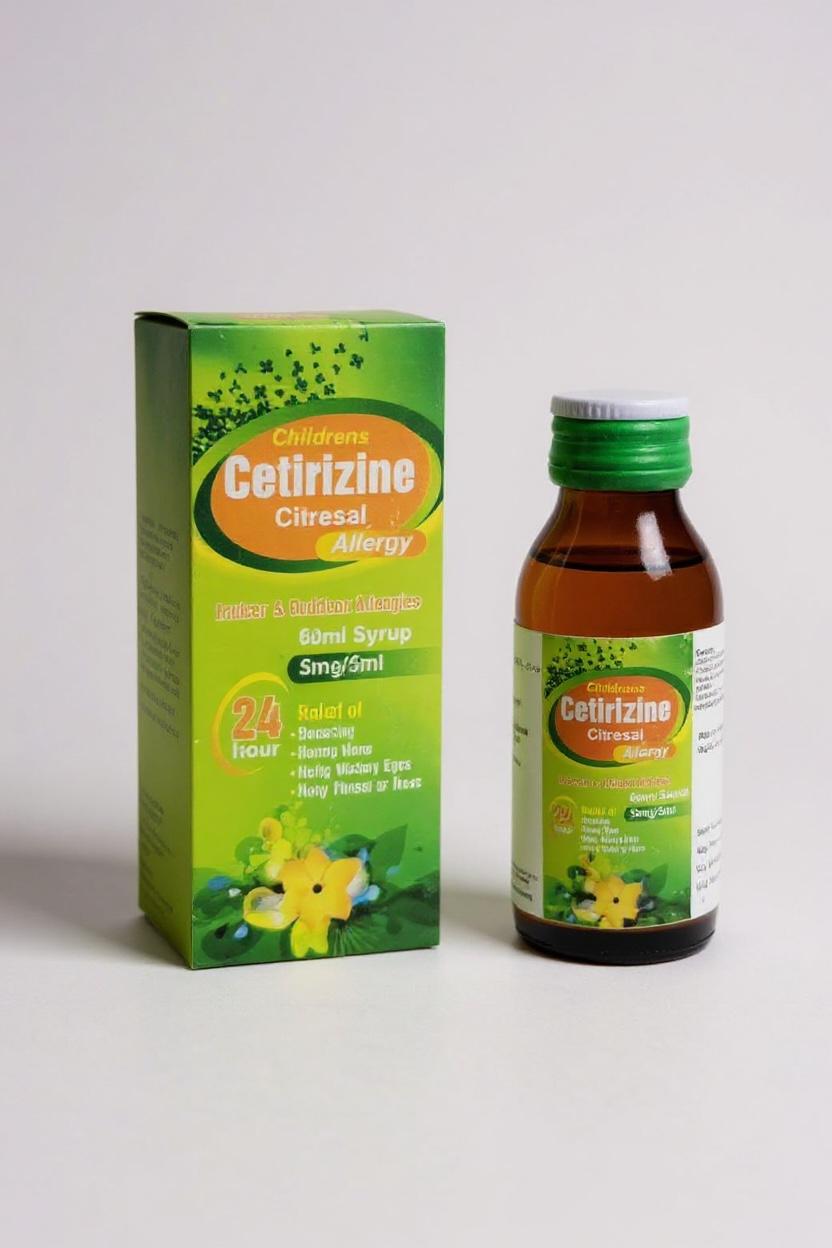
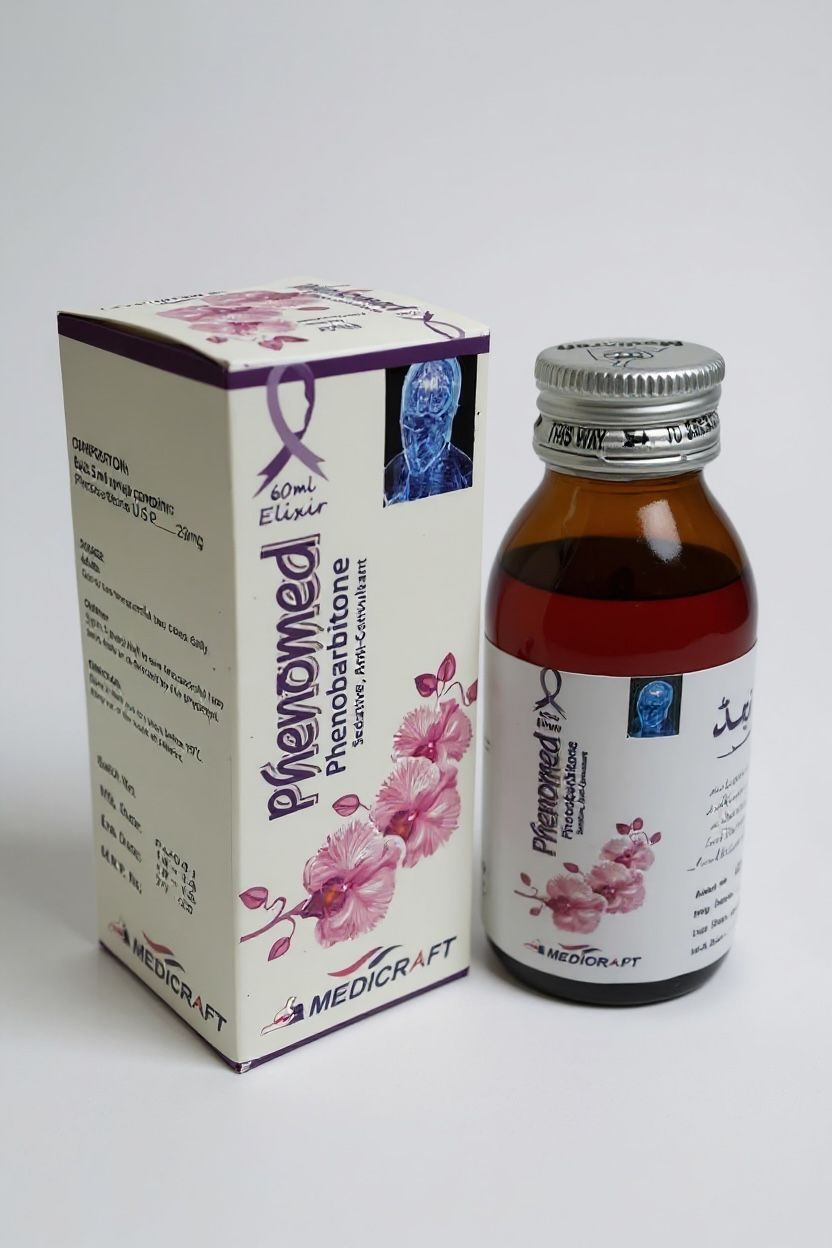
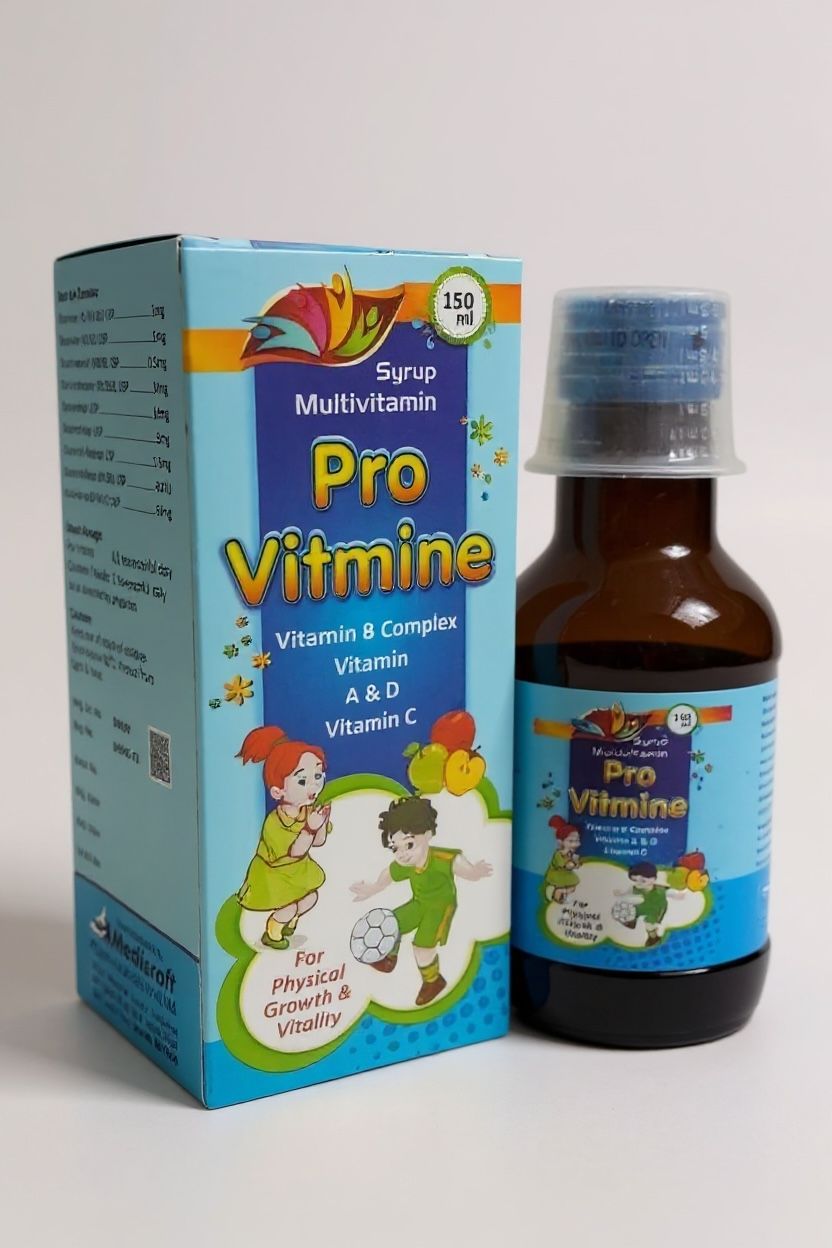
Our packaging process is just as excellent as the formulation. Each syrup is sealed with tamper-proof closures and child-resistant caps to prevent accidental ingestion.
Calibrated measuring cups or spoons are included with every unit to support accurate dosing by healthcare professionals and caregivers.
Labels are designed for clarity and compliance, displaying batch numbers, expiry dates, storage guidelines, and dosage instructions in accordance with regulatory norms.
Regional Supply Chain and Distribution
Our robust logistics network makes sure that every batch of liquid syrup reaches healthcare providers in optimal condition and on schedule. With temperature-controlled transport systems and centralized warehousing, we maintain the integrity of even the most sensitive formulations during transit.
Our distribution footprint spans Afghanistan, Pakistan, Kyrgyzstan, and Tajikistan, where we collaborate with hospitals, pharmacies, and government health departments to offer continuous product availability.