Packaging Integrity and Stability Assurance
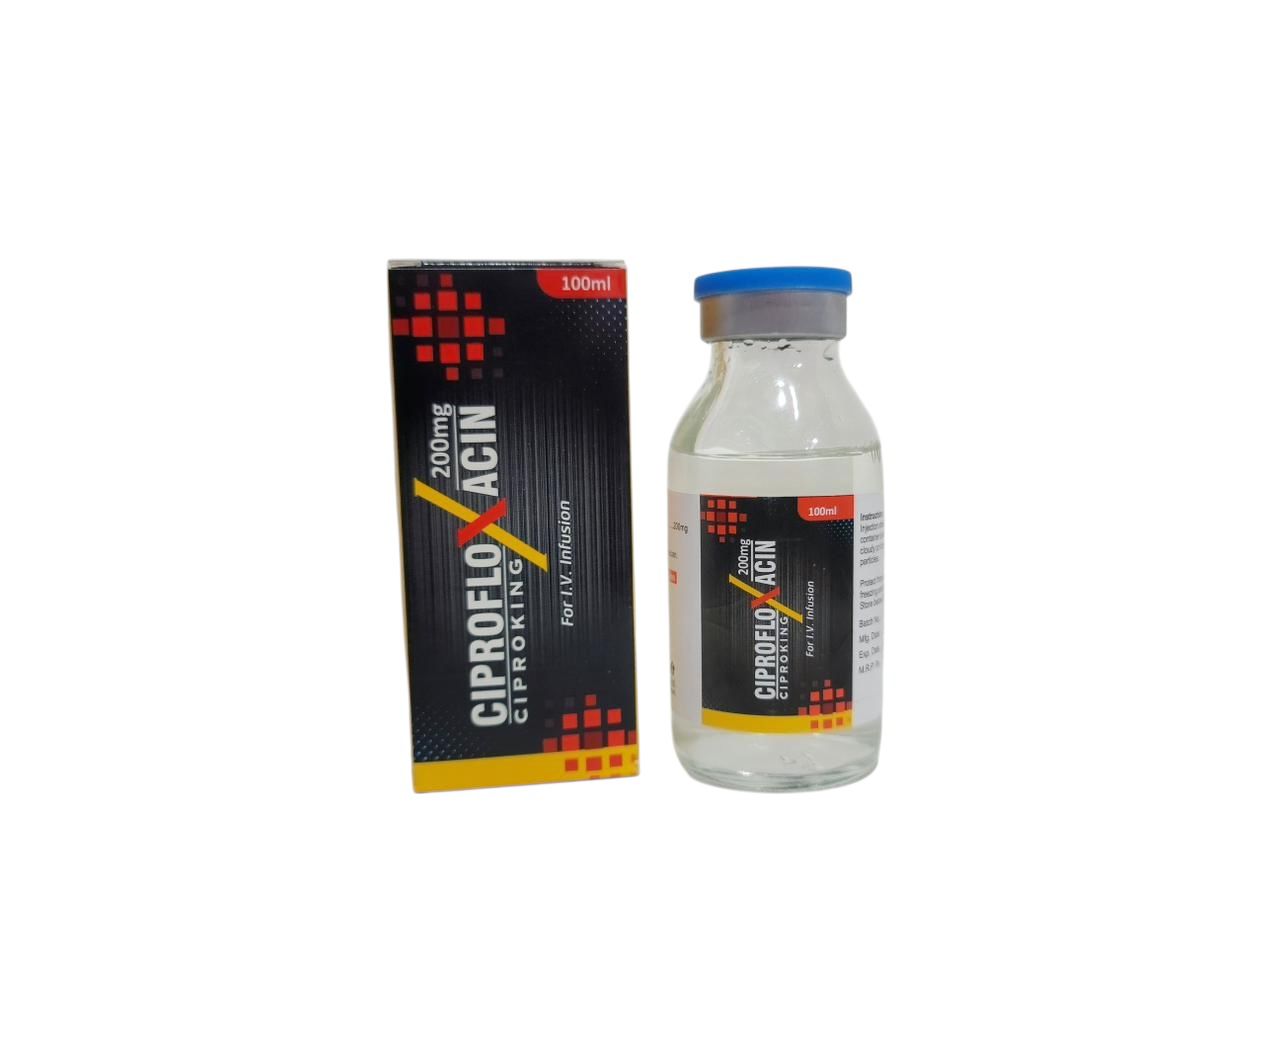
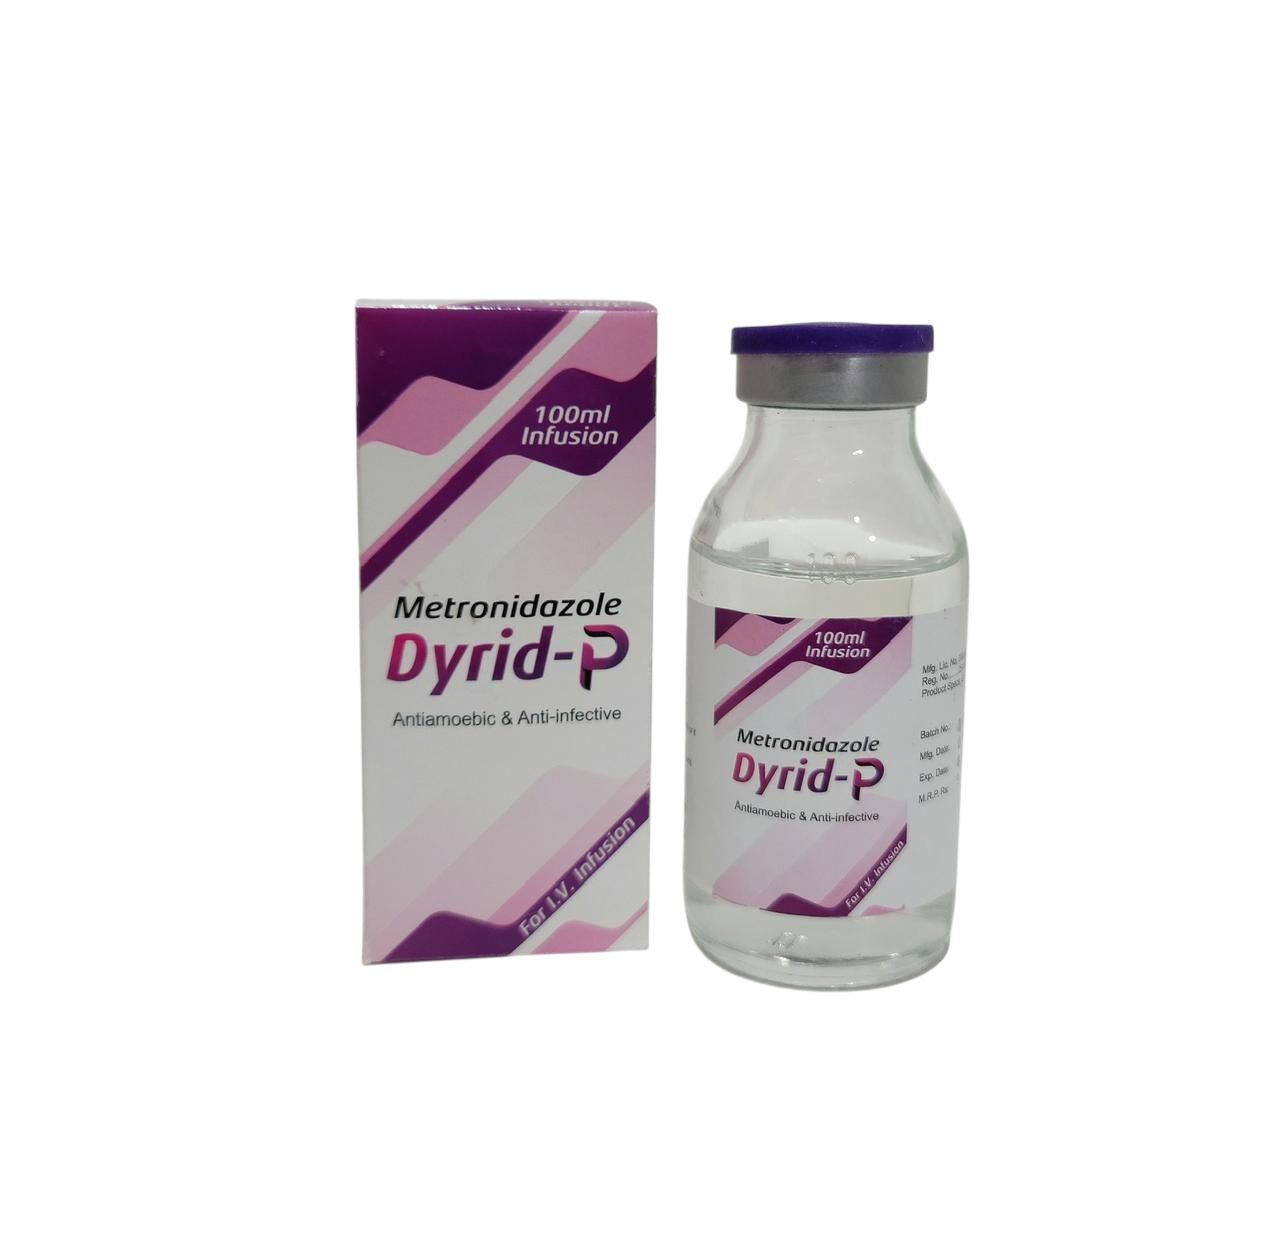
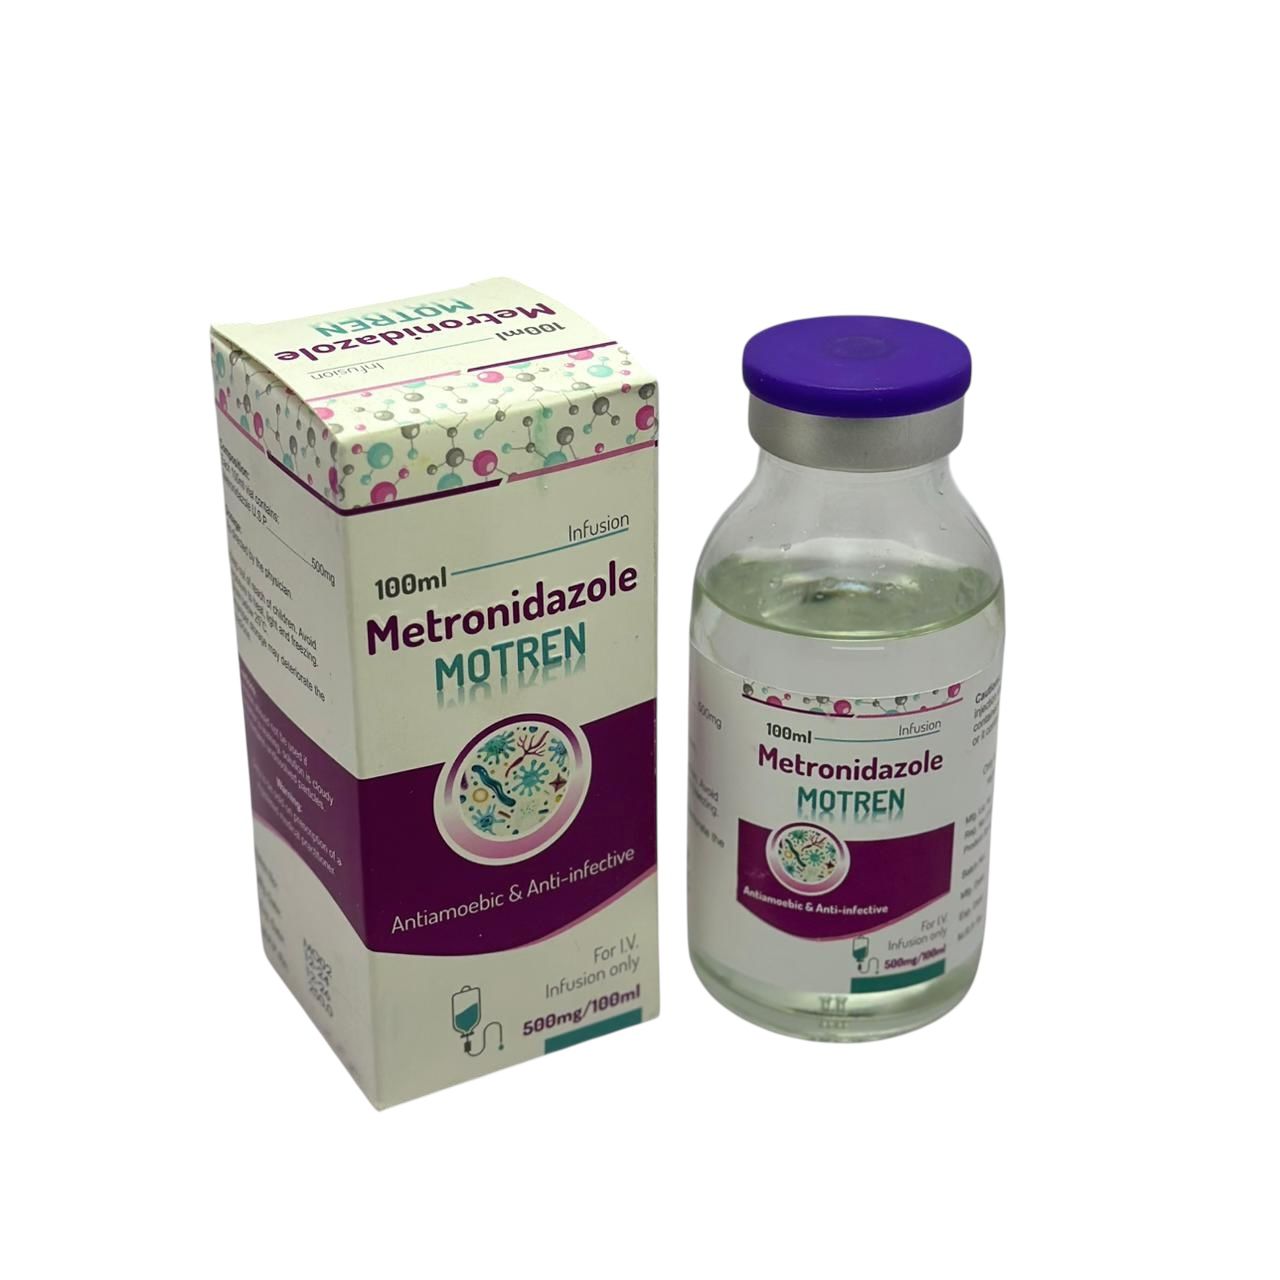
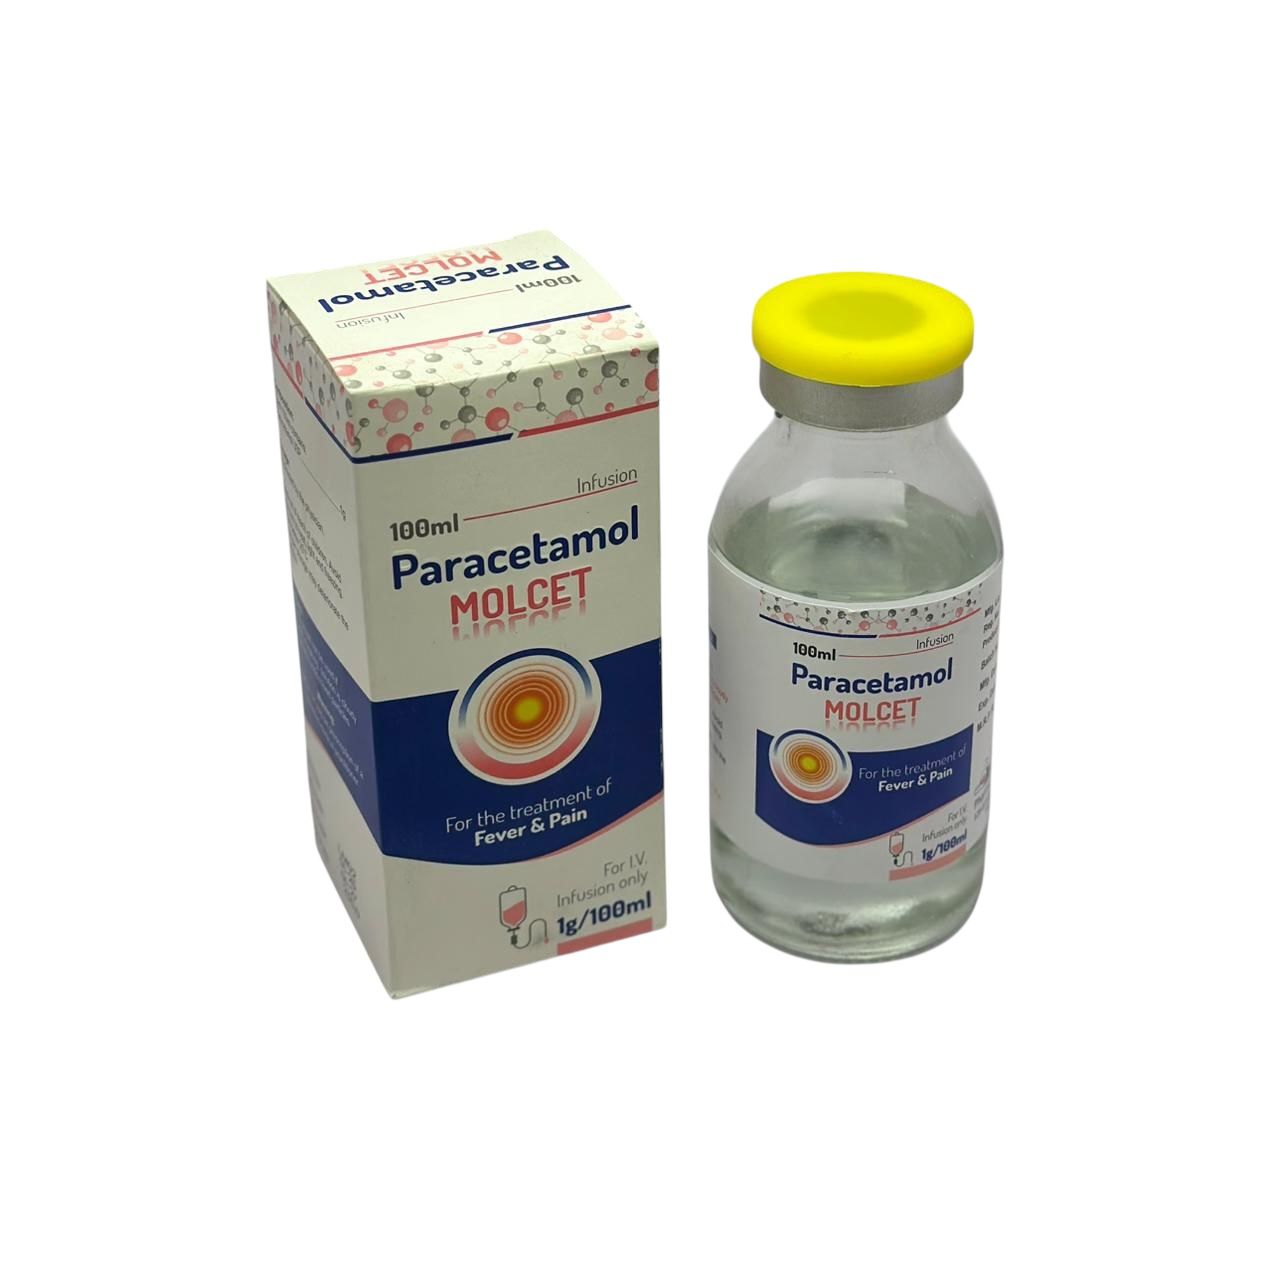
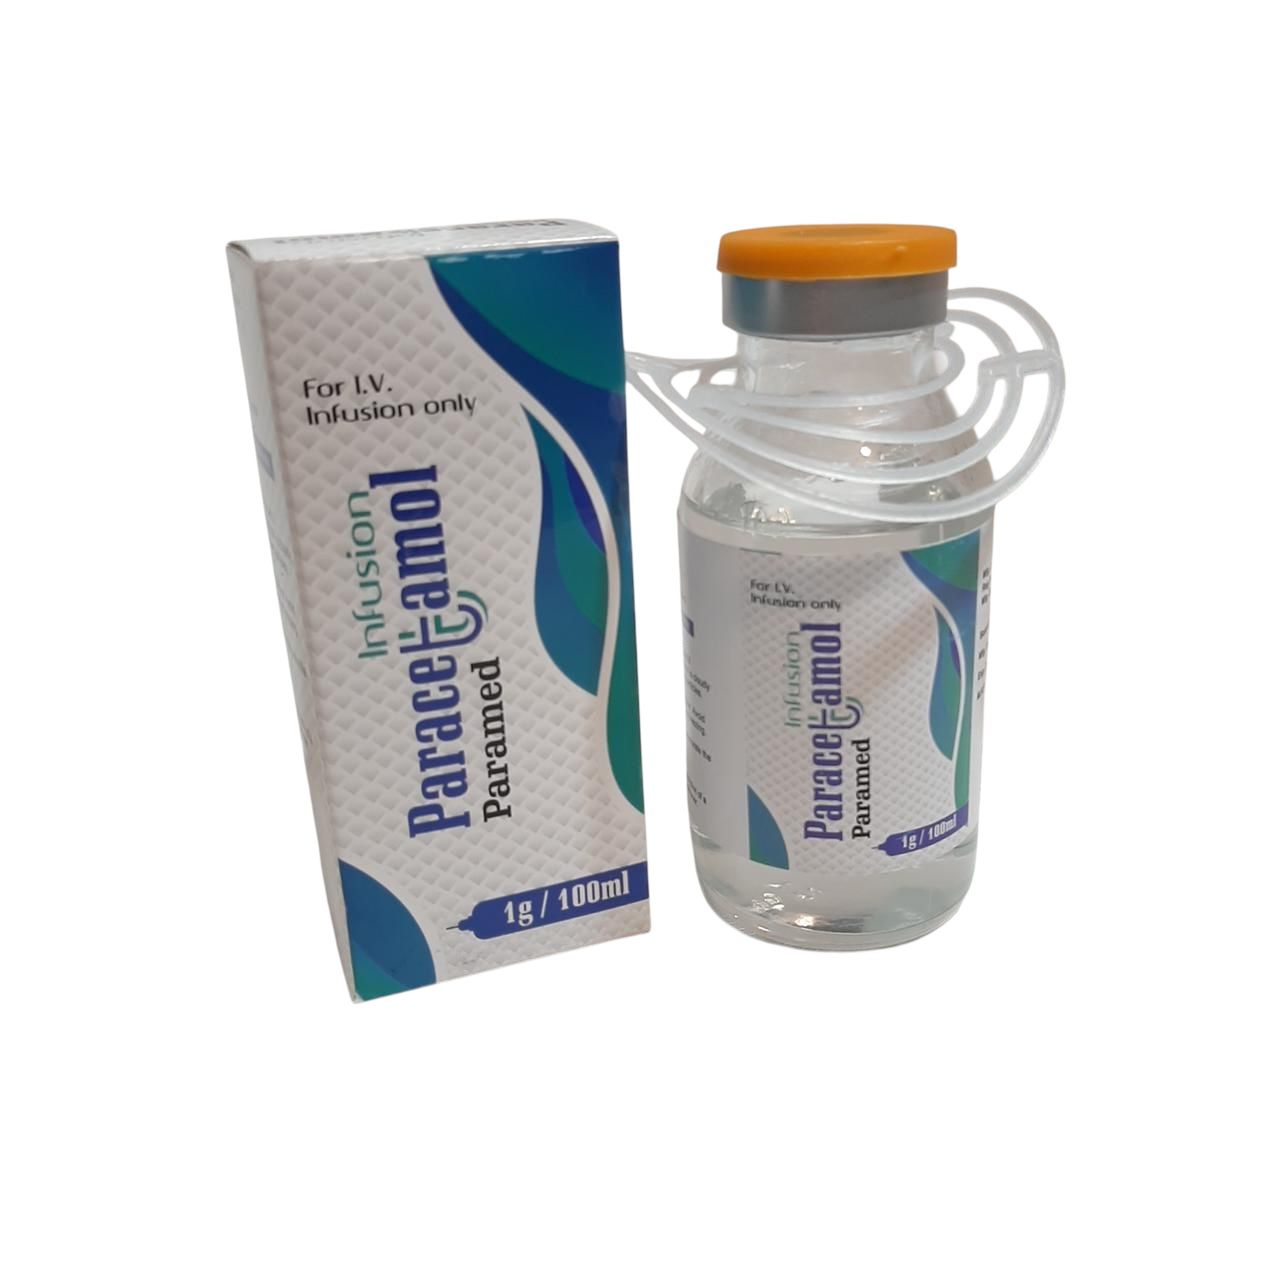
Each vial is constructed from pharmaceutical-grade borosilicate glass, sealed with butyl rubber stoppers, and crimped with aluminum caps to prevent contamination and moisture ingress.
For temperature-sensitive drugs, secondary protective packaging and insulated cartons are used to safeguard against environmental variations. Labels include lot numbers, expiry dates, reconstitution instructions, and storage guidelines, making sure that healthcare professionals can administer these products safely and efficiently.
To guarantee stability under regional conditions, all dry vial formulations undergo accelerated and long-term stability testing in simulated climates reflective of Afghanistan, Pakistan, Kyrgyzstan, and Tajikistan.
Distribution, Accessibility, and Supply Chain Management
We maintain a robust pharmaceutical distribution network designed to handle the specialized logistics required for dry vial transport. Warehouses are climate-controlled, monitored for humidity and temperature, and equipped with automated tracking systems.
Our supply chain follows GDP (Good Distribution Practice) standards, with each shipment accompanied by full documentation for customs, import authorities, and healthcare institutions. This makes sure that hospitals, pharmacies, and clinics across our service areas receive these sensitive products on time and in optimal condition.
To further support healthcare providers, we offer technical assistance and training on safe reconstitution, dosage accuracy, and administration methods.
Affordability, Trust, and Collaboration
Our approach is driven by the mission to make high-quality injectable treatments accessible and affordable. Through strategic partnerships with Seerat & Sarwat Pvt. Ltd. and Hasrat Rafiq Trading Company, we leverage decades of experience in pharmaceutical importation, regulatory compliance, and hospital supply chains.
These partnerships allow us to negotiate competitive pricing without compromising quality, helping healthcare facilities reduce procurement costs while maintaining therapeutic standards.
Commitment to Quality and Patient Care
Our dry vial range represents the perfect balance of scientific innovation, manufacturing precision, and clinical dependability. From lyophilization to delivery, every step reflects our commitment to promoting patient well-being and healthcare system efficiency.
We continue to expand our product portfolio, invest in advanced cold-chain logistics, and maintain full alignment with international healthcare regulations. Through continuous improvement and unwavering quality standards, our dry vials stand as a trusted resource for healthcare institutions across multiple regions.
Disclaimer:
All dry vial formulations must be used under the supervision of qualified healthcare professionals. Reconstitution, dosage, and administration procedures should always be followed as directed by a licensed physician or pharmacist. This content is for informational and professional reference only and does not replace medical consultation or prescription advice.